Beaker Brush
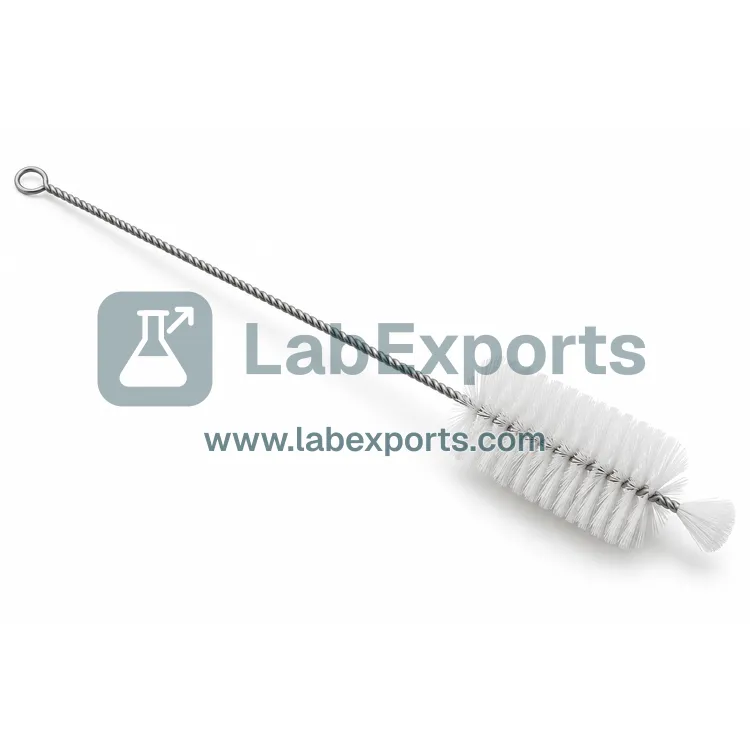
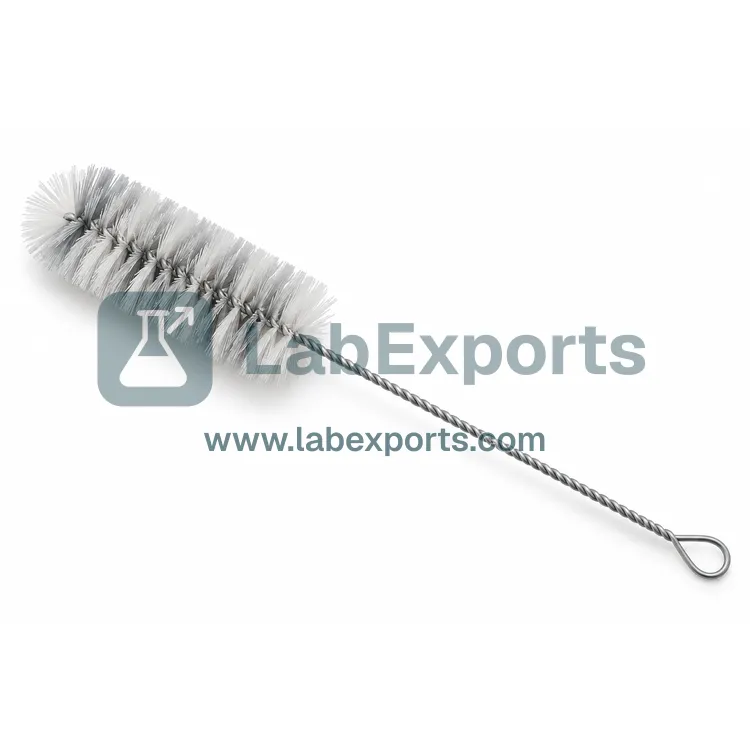
Beaker Brush: hard nylon bristles on twisted G.I. wire, head 140 x 63 mm, overall length 400 mm.
Equipping a new lab or bidding on a tender? Our sales team quotes volume orders directly.
Government & Tender Supply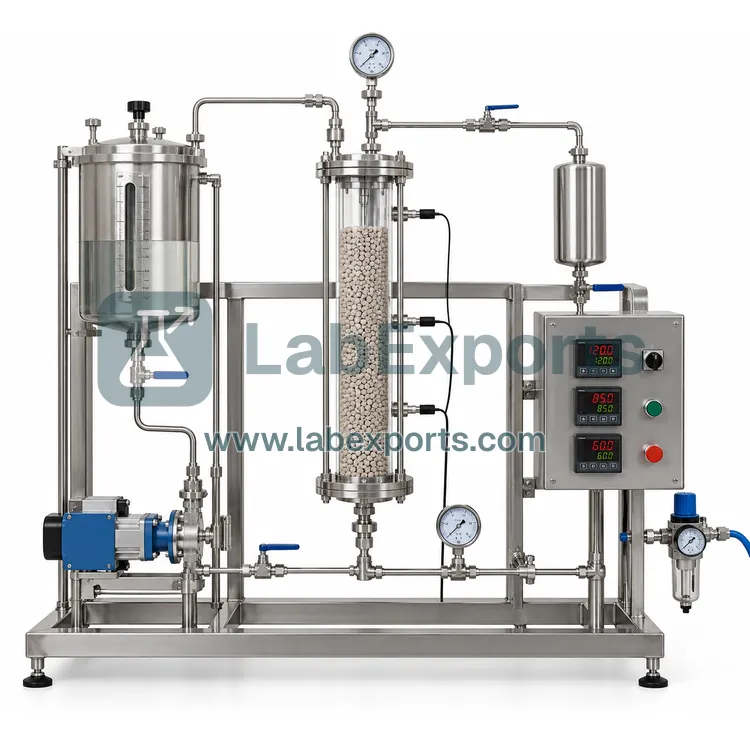
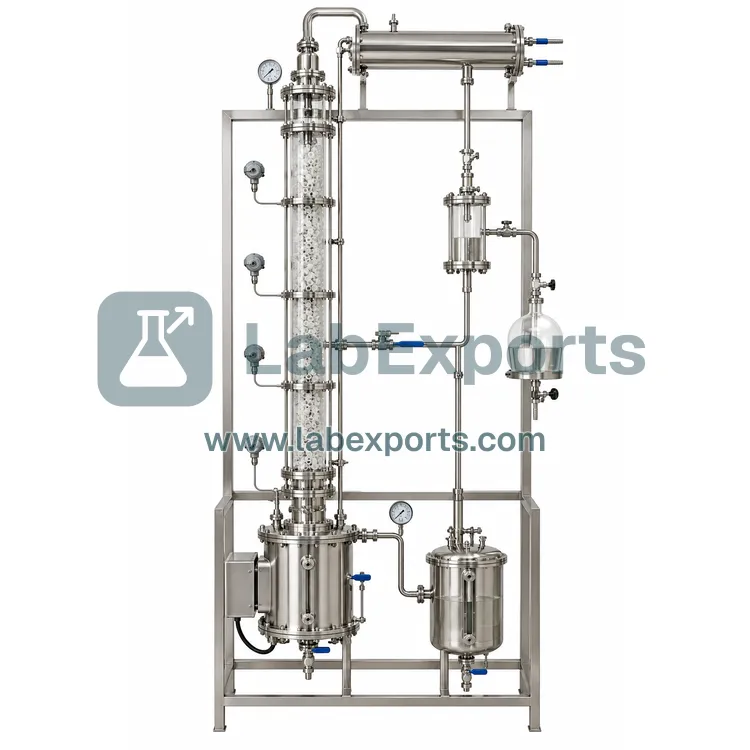
Packed Bed Reactor comprises of their high conversion rate per catalyst weight compared to other catalytic reactors.
Packed Bed Reactor Packed Bed Reactor comprises of their high conversion rate per catalyst weight compared to other catalytic reactors. These reactors are used in chemical processing applications such as absorption, distillation, stripping, separation processes, and catalytic reactions. This reactor contains a chamber, such as a tube or channel that contains catalyst particles or pellets, and a liquid that flows through the catalyst. Contact us for more details. Specification